


Introduction
Mixing is not just about turning a shaft. In viscous dairy, beverage, and food vessels, the right agitator must create the right flow pattern at the right power density, or the batch ends up stratified, overheated, or poorly blended. Power density—kilowatts per cubic metre of batch volume—is the simplest way to compare agitation intensity, and impeller flow pattern decides whether the fluid moves axially, radially, or tangentially. This guide covers how to choose both for viscous mixing vessels.
Power Density in kW/m³
Power density is the agitator power divided by the batch volume. It is a rough but useful measure of mixing intensity:
| Application | Typical power density |
|---|---|
| Gentle blending, low-viscosity liquids | 0.1–0.3 kW/m³ |
| Standard mixing, milk, juice | 0.3–0.8 kW/m³ |
| Homogeneous suspension, sauces | 0.8–1.5 kW/m³ |
| High-viscosity pastes, doughs | 1.5–3.0+ kW/m³ |
Power density alone is not enough; it must be paired with the right impeller and speed. A high-power density with the wrong flow pattern creates swirl and dead zones instead of blending.
Impeller Types and Flow Patterns
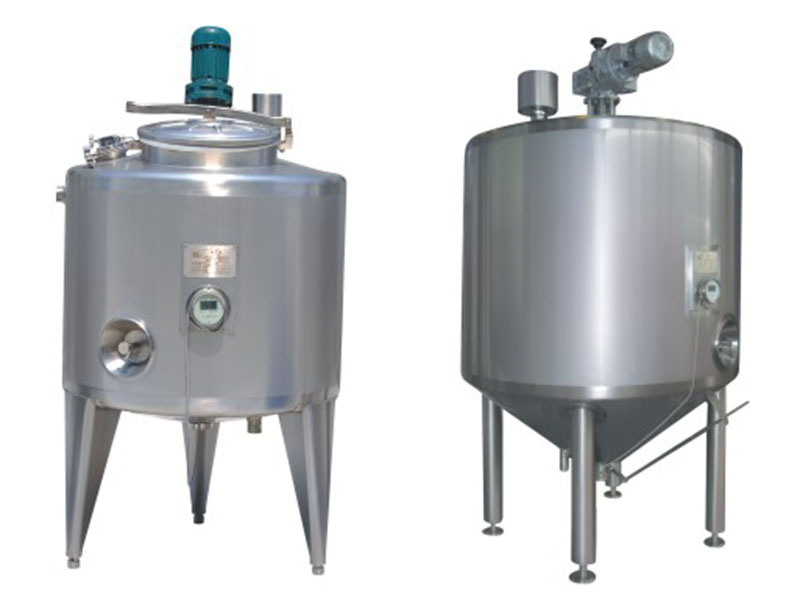
Axial-Flow Impellers
Propellers and pitched-blade turbines push fluid down or up along the shaft. They are efficient for blending, solid suspension, and heat transfer in low-to-medium viscosity fluids. They need baffles to prevent swirling.
Radial-Flow Impellers
Flat-blade turbines discharge fluid outward toward the vessel wall, creating top-to-bottom circulation. They provide good shear at the blade and are useful for gas dispersion, liquid-liquid dispersion, and high-shear zones.
Tangential and Anchor Impellers
Gate, anchor, and helical impellers sweep close to the wall. They prevent wall build-up in viscous products like caramel, yogurt, and tomato paste but create little axial circulation on their own.
Laminar vs Turbulent Flow
The Reynolds number for agitation is Re = ρND²/μ, where N is impeller speed (rev/s), D is impeller diameter, and μ is viscosity. For water-like fluids Re is high and flow is turbulent; for viscous sauces Re drops below 10 and flow is laminar. In laminar flow, baffles do little and anchor or helical impellers become necessary. In turbulent flow, baffles and axial impellers dominate.
Viscous Mixing Considerations
As viscosity rises, the fluid no longer moves in large circulatory loops. Instead, mixing happens by direct shear and wall scraping. High-viscosity impellers need:
- Large diameter (often 0.7–0.9 of tank diameter).
- Low speed to avoid motor overload.
- Close wall clearance to prevent stagnant layers.
- Helical or anchor geometry for top-to-bottom turnover.
Baffles and Draft Tubes
Baffles stop swirling and convert rotational motion into vertical mixing. For low-viscosity fluids, four wall baffles are standard. In viscous batches, baffles can create dead zones, so a draft tube around the impeller is sometimes better—it forces axial flow through the centre and back up the wall. Draft tubes are common in crystallization and suspension duties.
Scale-Up Rules
When moving from pilot to production, keep one parameter constant and accept changes in others. Common scale-up rules:
- Constant tip speed: ND scales with D.
- Constant power per volume: P/V stays the same.
- Constant Reynolds number: N scales with 1/D².
For geometrically similar tanks, constant power per volume is the safest default for blending, though it may over-shear the product at large scale. Always test scale-up assumptions with a production trial.
Specifying an Agitator
Provide the supplier: tank volume, product viscosity and density, mixing duty (blend, suspend, heat, dissolve, emulsify), target batch time, allowable temperature rise, and whether CIP must reach all surfaces. The agitator tank supplier then selects impeller type, diameter, speed, motor power, and baffle configuration to hit the required power density and flow pattern.
Common Mistakes
- Specifying only horsepower. A 5 kW agitator with the wrong impeller performs like a 1 kW one.
- Using a propeller in viscous paste. The impeller creates a local vortex and leaves the rest stagnant.
- No baffles in low-viscosity tanks. The whole batch swirls with almost no mixing.
- Ignoring viscosity changes. A product that thickens during heating needs a different impeller than when cold.
FAQ
What is a typical kW/m³ for milk mixing?
0.3–0.8 kW/m³ for general mixing; higher if the duty involves powder incorporation or temperature uniformity.
Which impeller for high-viscosity sauce?
Anchor, gate, or helical impellers that sweep the wall and move product top-to-bottom.
Do I need baffles?
Yes for low-to-medium viscosity. For very viscous products, use a wall-scraping impeller instead of baffles.
How do I scale up from pilot?
Keep power per volume constant for blending; keep tip speed constant if shear-sensitive. Run a production trial to confirm.
Can one agitator do blending and heating?
Yes, with the right flow pattern. Axial impellers give good heat-transfer coefficients at the jacket wall by sweeping the surface.
Conclusion
Power density and impeller flow pattern are the two levers that decide whether a mixing vessel actually blends. Low-viscosity milk and juice respond to axial impellers with modest power density; viscous sauces and pastes need wall-sweeping impellers and higher power density. Specify the duty first—blend, suspend, heat, or emulsify—then match the impeller and kW/m³ to the viscosity. A well-matched agitator tank saves batch time, improves heat transfer, and eliminates the dead zones that ruin product uniformity.