


Introduction
Shelf-stable food and beverage products rely on a documented lethal dose of heat, not just a temperature setpoint. That dose is expressed as F0, the equivalent minutes at 121 °C. Get F0 wrong and you either under-process and risk spoilage, or over-process and destroy color, texture, and nutrients. This guide explains how F0 is calculated, how a water bath sterilizer achieves it, and what to validate before releasing the first batch.
What F0 Means in Practice
F0 is a lethality unit that compares the actual time-temperature history of the coldest spot in the product to the lethality of 121 °C. The reference organism is Clostridium botulinum, with a z-value of 10 °C, meaning the lethal rate doubles for every 10 °C rise. A process with F0 = 5 minutes at the cold spot delivers the same lethality as holding at 121 °C for 5 minutes. Commercially sterile low-acid foods typically target F0 ≥ 3–5, while many dairy and beverage applications settle at F0 5–10 to build margin.
The F0 Formula
The calculation integrates lethal rate over time:
F0 = ∫ 10(T − 121)/10 dt
Where T is the cold-spot temperature at time t. In practice the integral is replaced by a summation using logged data points every 30–60 seconds:
F0 = Σ 10(T − 121)/10 × Δt
At 100 °C the lethal rate is 0.008; at 115 °C it is 0.25; at 121 °C it is 1.0. This is why the last few degrees below 121 °C contribute so little—most lethality accumulates during the plateau near sterilization temperature.
How a Water Bath Sterilizer Achieves F0
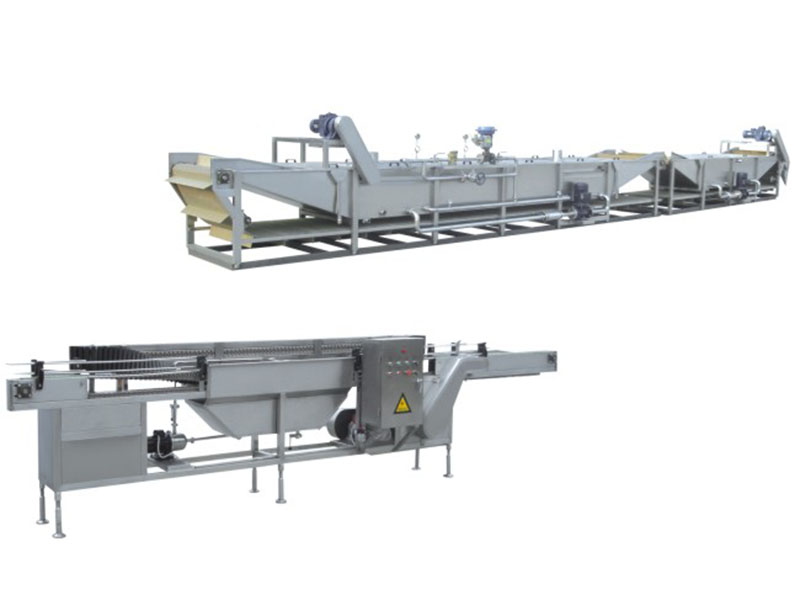
A water bath sterilizer immerses sealed containers in a bath of pressurized hot water. Because water transfers heat much faster than steam condensing in a still retort, and because the water is actively circulated, the temperature profile around each pack is uniform. Once the cold spot in the slowest-heating container reaches the target temperature, the hold timer begins. The F0 value is then accumulated over the hold plus the slow cooling phase, until the cold spot drops below a cut-off such as 100 °C.
Water Bath vs Static Retort
| Factor | Water Bath Sterilizer | Static Steam Retort |
|---|---|---|
| Heat transfer | Forced hot-water circulation | Steam condensing |
| Temperature uniformity | High | Moderate |
| Over-pressure control | Excellent for pouches | Moderate |
| Come-up time | Fast | Slower |
| Best for | Pouches, trays, glass, cans | Cans, jars |
Calculating F0 for a Water Bath Cycle
A typical cycle has five phases: come-up, hold, sterilization plateau, cooling, and ambient drain. Loggers are placed in the slowest-heating container at the geometric cold spot—usually the centre of the largest, most viscous pack. The F0 sum includes only the portions above the cut-off temperature. A practical example:
- Cold spot reaches 121 °C after 12 minutes come-up.
- Hold at 121 °C for 8 minutes.
- Slow cooling through 110–100 °C adds another ~1.2 minutes equivalent.
- Total F0 ≈ 9.2 minutes → exceeds target of 5.
If the product is viscous, the cold spot may not reach bath setpoint until late in the hold; the hold time must then extend to compensate.
Cold Spot Determination
The cold spot is not always the geometric centre. For a still liquid it is usually the centre; for a viscous sauce or a particulate soup it shifts toward the thickest, slowest-heating region. Validation requires thermocouples or wireless loggers distributed across multiple containers in the worst-case location—typically the centre of the load and the corners of the crate. Once the cold spot is mapped, the production logger is placed there for every validation batch.
Counter-Pressure for Fragile Packs
As packs heat, internal pressure rises. Without external counter-pressure, flexible pouches balloon and may burst, while glass jars can crack from internal pressure against the closure. Water bath sterilizers control this by maintaining an air over-pressure above the water, balancing the pressure differential across the package. Counter-pressure is essential for retort pouches and thin-wall trays and is one reason water baths dominate these formats.
Validation and Process Logging
Regulators and customers require documented evidence. A validation protocol should include: heat-penetration studies on the slowest-heating product and pack, cold-spot mapping, repeat runs to confirm, calibration certificates for loggers and pressure gauges, and a detailed process file specifying bath temperature, hold time, over-pressure setpoint, and cooling parameters. Once validated, production runs need batch records with continuous temperature and pressure charts.
Common Mistakes
- Using bath temperature instead of cold-spot temperature. The process must be calculated at the product cold spot, not the water bath.
- Ignoring come-up and cooling. These phases can add or subtract significant F0.
- Choosing one logger location. Without mapping, you may miss the true cold spot.
- Skipping counter-pressure. Pouches will fail validation if they deform or burst.
FAQ
What is the minimum acceptable F0?
For low-acid foods, F0 ≥ 3 minutes is the legal minimum; most commercial processes use 5–12 minutes to provide margin and account for variation.
Can I use a water bath for retort pouches?
Yes—water bath sterilizers with counter-pressure are the standard method for retort pouches and trays because they prevent deformation.
How many thermocouples do I need for validation?
At minimum 10–12 distributed across the load, including the geometric centre, corners, and one in the slowest-heating container. Repeat three runs.
Does cooling contribute to F0?
Yes, while the cold spot is above ~100 °C the lethal rate is still accumulating, though much more slowly than at 121 °C.
What logger interval should I use?
Every 30–60 seconds is standard; faster intervals (10–15 s) improve accuracy for short cycles or viscous products.
Conclusion
F0 is the only number that proves a shelf-stable product is safe. A water bath sterilizer gives you the uniform heat and counter-pressure control needed to hit that number consistently. Calculate it from the cold-spot temperature log, validate it across repeated runs, and document it for every batch. Do that, and the retort or water bath becomes a precision lethality machine rather than a simple heater.