Introduction
Milk rarely moves through a dairy plant as one smooth, continuous stream. The pasteurizer runs at a steady rate; the filler works in cycles; fermentation waits for no one, and CIP stops everything. Different stages pull product at different speeds, and some run continuously while others work batch by batch.
A buffer tank is the piece of equipment that absorbs this mismatch.
Placed between two stages, it holds product temporarily so upstream and downstream machines don’t have to run in perfect lockstep. In practice, that means steadier flow, cleaner separation between production stages, fewer interruptions at the filler, and less start-stop chaos across the line.
You’ll find buffer tanks in milk processing, yogurt production, cream handling, cheese plants, and most other liquid food operations. Compared with a pasteurizer or an evaporator, the vessel itself looks almost trivial — a stainless steel tank, some connections, maybe an agitator. But its size, its configuration, and where it sits in the line have an outsized effect on how the whole plant runs.
And that’s the trap: a buffer tank is not a “bigger is safer” purchase. This guide walks through what these tanks actually do, how to size one properly, and what to specify before you order.
What Is a Buffer Tank in Dairy Processing?
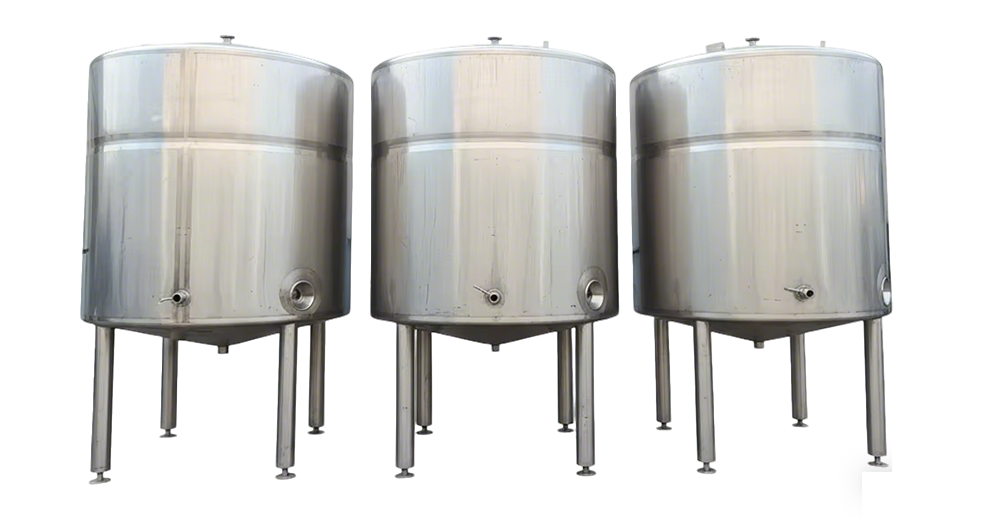
A buffer tank is a sanitary process vessel that holds liquid product temporarily between two production stages.
Its job is to decouple those stages.
Take a pasteurizer running continuously at a fixed flow, feeding a filling machine that works on its own production cycle. Between them, a buffer tank absorbs the short-term differences — product flows in from upstream whether or not the filler is ready for it, and flows out whenever the filler asks.
Instead of every machine starting and stopping together, the tank holds a controlled volume of product that downstream equipment can draw on.
Depending on the application, dairy plants use buffer tanks for:
- Temporary product storage
- Flow stabilization
- Batch separation
- Product transfer
- Filling-line supply
- Fermentation process support
- Ingredient or intermediate-product holding
- Production changeover management
The vessel alone doesn’t do any of this. Pumps, valves, pipelines, level sensors, temperature controls, and CIP connections all have to work with the tank as one system.
Why Are Buffer Tanks Important in Dairy Processing?
-
They balance different processing speeds
No two machines on a dairy line run at exactly the same rate, and that is the quietest source of trouble in plant design.
Picture a pasteurizer producing 5,000 L/h while the filling line downstream draws product at its own pace. Without buffering, every mismatch forces an adjustment or an interruption.
A buffer tank holds a temporary reserve between the two. Upstream keeps running while downstream catches up, and nobody has to throttle anything.
-
They reduce unnecessary production stops
A brief hiccup in one corner of the line shouldn’t stop the whole plant, but without buffering it usually does.
If a filling machine stops for a quick adjustment while upstream processing continues, a properly sized tank simply takes the product. The same logic runs in reverse: when upstream goes down, the filler can keep drawing from the buffer for a while.
Line utilization goes up, and short interruptions stop being line-wide events.
-
They support continuous and batch processing
Most dairy plants mix operating modes. Pasteurization is continuous; formulation, fermentation, and flavoring happen in batches.
A buffer tank is the practical bridge between the two — and it matters most in yogurt and cultured dairy production, where fermentation timing and filling schedules rarely line up neatly.
-
They help manage product changeovers
A dairy plant may run several products in a single day — plain yogurt in the morning, flavored yogurt after lunch. Buffer tanks create separation between batches and provide controlled holding during the switch.
One caution: changeover and cleaning are the same problem. A bigger tank does not automatically make changeovers easier, because there is more surface to clean and more product at risk.
Common Applications of Dairy Buffer Tanks
The right design depends on what the tank is expected to do.
Milk buffer tanks sit between receiving, pasteurization, homogenization, and other stages, smoothing flow and holding product when adjacent stages run at different rates.
Yogurt buffer tanks have a harder job. After fermentation the product structure is fragile, and excessive shear ruins texture. Between fermentation, cooling, mixing, and filling, the tank and transfer system must be chosen to handle the product gently.
Cream and other dairy liquids bring different viscosities and handling behavior than plain milk. Tank design should follow the product, not the other way around.
Beverage and liquid food processing uses the same buffering principle outside dairy altogether. Zhongbo manufactures stainless steel process tanks for food, dairy, beverage, pharmaceutical, and other hygienic applications, so buffer-tank concepts carry over into broader liquid-processing systems.
What Is the Difference Between a Buffer Tank and a Storage Tank?
The two get mixed up constantly, but they do different jobs.
A storage tank holds product for a long time — raw milk waiting for processing, finished product waiting for distribution.
A buffer tank manages flow between processing stages. It lives in the middle of the process, not at either end of it.
In a typical line:
Raw milk storage → Pasteurization → Buffer tank → Filling
The raw milk tank stores before processing; the buffer tank keeps the pasteurizer and the filler from fighting each other. A buffer tank often holds a relatively small working volume, because its purpose is to absorb short-term variation, not to warehouse product.
How to Size a Dairy Buffer Tank
Sizing is where most buffer tank projects are won or lost.
Start with two numbers: required buffer time and process flow rate.
Buffer Volume = Flow Rate × Required Buffer Time
Example: a line handling 4,000 L/h with 15 minutes of buffering needs
4,000 L/h × 15/60 h = 1,000 L
That is a theoretical volume of roughly 1,000 liters. Don’t order a 1,000 L tank yet.
A process tank needs headspace and should not run at 100% of its geometric volume. The final specification has to account for working volume, headspace, operating range, level control, and how the process actually behaves on the floor — not just on paper.
Working Volume vs. Total Tank Volume
This is where specification sheets mislead people.
Suppose a tank has a total geometric volume of 1,500 L. That is not 1,500 L of working capacity. The usable volume is lower, because the tank needs room for:
- Headspace
- Level fluctuations
- Product movement
- Foam
- CIP requirements
- Safe operation
- Instrumentation and control
When you request a quotation, make the manufacturer state total volume and working volume separately. It is a small question that prevents a very common purchasing mistake.
How Much Buffer Time Do You Need?
There is no universal answer. The right buffer time depends on what problem the tank is solving:
- How often does the downstream process stop?
- How long do typical interruptions last?
- Is the upstream process continuous?
- Is the downstream process batch-based?
- How quickly can operators respond to an interruption?
- Does the tank need to cover minutes of buffering, or longer intermediate storage?
A tank smoothing out filling-speed fluctuations is a very different animal from one holding product through a long production transition.
Aim for the minimum practical buffer capacity that stabilizes the process. Maximizing volume is not the goal; it is usually the mistake.

Factors That Affect Buffer Tank Sizing
Flow rate and buffer time get you started. They don’t get you finished.
- Product flow rate. Establish both normal and maximum flow. A line running 3,000 L/h normally with occasional peaks of 5,000 L/h has to be sized against both numbers.
- Upstream and downstream capacity. Compare the equipment on either side. If a pasteurizer supplies 5,000 L/h and the filler consumes 4,000 L/h, the buffer tank fills steadily unless someone adjusts the rates. No tank fixes a fundamental capacity imbalance — it only postpones it.
- Batch size. When the tank supports batch processing, required volume may follow the batch, not the line flow.
- Product characteristics. Milk, cream, yogurt, concentrates, and flavored products behave differently. Viscosity, solids, foaming, and shear sensitivity all shape the tank design and the transfer system.
- Residence time. Some products care how long they wait. If holding time affects quality, extra buffer capacity creates a new problem: product sitting longer than it should. Bigger is not better here.
- Future expansion. If production will grow, plan for it early — but think twice before oversizing today. Extra volume raises capital cost and extends residence time. Often the smarter move is designing the layout and connections so capacity can be added later.
Key Design Features of a Sanitary Dairy Buffer Tank
A dairy buffer tank does more than hold liquid.
Stainless steel construction. Food and dairy vessels use stainless steel suited to hygienic service. Internal surface finish and construction details should follow the product and the applicable hygiene standards.
Sanitary connections. Product-contact connections, valves, outlets, and pipelines should minimize contamination risk and clean effectively.
Appropriate agitation. Not every tank needs an agitator, and few need an aggressive one. Match the agitator to viscosity and product characteristics — for delicate products, excessive shear is a defect, not a feature.
Level measurement. Accurate level monitoring is what lets the control system know how much product is available and prevent overflow or pump starvation.
Temperature control. Some applications need the product held within a controlled temperature range, which means heating or cooling on the tank. Zhongbo offers stainless steel process tanks with customizable configurations, including heating and cooling arrangements. (zjzhongbo.com)
CIP compatibility. Design for cleaning from day one. Spray device, internal geometry, valves, outlets, pipelines, and dead-leg control all determine how well the tank cleans. In dairy, CIP is part of the tank design, not an accessory bolted on later.
Buffer Tank Design and CIP
Dairy products are unforgiving cleaning targets. Milk leaves protein, fat, and mineral deposits on every product-contact surface.
Effective CIP means getting the right flow, chemical concentration, temperature, and cleaning time to the surfaces that need them — which is why the tank and the CIP system should be designed together.
Work through:
- Spray ball or rotary spray device
- Tank geometry
- Product outlet design
- Valve configuration
- Pipe routing
- Drainability
- Internal surface finish
- Cleaning flow rate
A tank that looks fine in a drawing but hides hard-to-clean corners will cost you in hygiene and maintenance for years. Zhongbo also supplies CIP equipment for dairy and food-processing applications, so cleaning can be engineered into the line as a whole. (zjzhongbo.com)
Should You Choose a Standard or Customized Buffer Tank?
If the application is straightforward, a standard tank does the job.
But dairy lines tend to have opinions. Capacity, tank dimensions, inlet and outlet positions, agitation, heating or cooling, level sensors, temperature sensors, CIP connections, automation, installation space — any one of these can force a custom build.
A customized tank makes sense when the vessel has to fit an existing line. What matters is not whether the tank holds the right number of liters; it is whether it fits the process, the layout, the utilities, the cleaning system, and the control strategy.
Common Buffer Tank Sizing Mistakes
Sizing capacity from daily production. A plant producing 50,000 L/day does not need a 50,000 L buffer tank. Size around process flow, interruption time, batch size, and residence time.
Treating total volume as working volume. Nominal capacity and usable capacity are different numbers. Always ask which one you are buying.
Ignoring the filling machine. The tank exists to serve the relationship between upstream and downstream equipment. Size it against that relationship, not in isolation.
Oversizing. A very large tank adds cost and residence time without adding much process benefit.
Forgetting CIP. The cleaning system has to reach every product-contact surface. If it can’t, nothing else about the tank matters.
How to Specify a Buffer Tank for Your Dairy Line
Before contacting a manufacturer, gather:
- Product: milk, yogurt, cream, beverage, etc.
- Product viscosity: preferably at relevant processing temperatures
- Normal flow rate: L/h
- Maximum flow rate: L/h
- Required buffer time: minutes
- Working volume: required usable capacity
- Product temperature: normal and maximum/minimum
- Agitation: required or not required
- Heating/cooling: required or not required
- CIP method: existing or new CIP system
- Installation space: available dimensions and orientation
- Automation: manual, semi-automatic, or automatic
- Future expansion: expected or not
Hand a manufacturer this list and you will get a useful quotation instead of a guess.
Q&A
Q1. What is the purpose of a buffer tank in dairy processing?
It holds dairy product temporarily between two processing stages, so flow rates and operating conditions on either side don’t have to match. The result is a line that runs more continuously.
Q2. How do I calculate the required buffer tank size?
Start with Buffer Volume = Flow Rate × Required Buffer Time. A 4,000 L/h process needing 15 minutes of buffering works out to about 1,000 L of working volume. From there, add allowances for headspace, operating range, product characteristics, and control requirements.
Q3. Is a larger buffer tank always better?
No. Extra volume means extra cost and longer residence time. Size for the interruption or imbalance you actually need to cover.
Q4. What is the difference between a buffer tank and a storage tank?
A storage tank holds product for longer periods; a buffer tank stabilizes flow between stages. The practical difference comes down to where the vessel sits in the process and what it is there to do.
Q5. Does a dairy buffer tank need an agitator?
Depends on the product. Some applications need gentle mixing to keep the product uniform; others don’t need agitation at all. Viscosity, solids content, and product sensitivity decide.
Q6. Can a buffer tank be heated or cooled?
Yes. Jackets or other heating/cooling arrangements are common when product temperature must stay within a range during holding.
Q7. How important is CIP for a dairy buffer tank?
Critical. In hygienic dairy processing, the tank, valves, pipelines, and internal surfaces must be designed so cleaning solutions reach every relevant product-contact area.
Q8. Can Zhongbo customize dairy buffer tanks?
Yes. Zhongbo builds stainless steel buffer and process tanks for dairy, food, beverage, pharmaceutical, and other hygienic applications. Capacity, configuration, heating or cooling, mixing, connections, and other features are designed to the project. (zjzhongbo.com)
Conclusion
Buffer tanks give dairy plants controlled flexibility between production stages — balancing flow rates, absorbing stops, bridging batch and continuous operations, and holding product before filling.
None of that comes from volume alone. Flow rate, buffer time, working volume, product characteristics, residence time, temperature control, agitation, CIP, and future plans all shape the right specification. The simple sizing formula is a starting point; the final tank should be designed around the whole process.
Zhongbo supplies stainless steel buffer tanks and related dairy processing equipment, with configurations adapted to different production requirements. Combined with sanitary pumps, CIP systems, mixing equipment, heat-treatment equipment, and other process machinery, they form part of an integrated dairy processing solution.
Planning a dairy processing line or replacing an existing buffer tank? Contact Zhongbo with your product, flow rate, required buffer time, and tank capacity to discuss a suitable sanitary tank solution.