Introduction
Choosing a pasteurization system takes more than picking the highest temperature or the newest heat exchanger. The right method depends on the product’s pH, viscosity, solids content, heat sensitivity, target shelf life, production capacity, packaging process, and required microbial reduction.
Milk, fruit juice, soy milk, oat beverages, and other plant-based drinks can all need thermal treatment, but they don’t behave the same way in the plant. A system that handles low-viscosity milk well may be a poor fit for a beverage with pulp, suspended particles, or a high solids load.
If you’re planning a new production line or upgrading an existing one, understanding these differences is the first step toward choosing between HTST, UHT, plate heat exchangers, tubular systems, and other pasteurization configurations.
Start With the Product, Not the Equipment
The most common mistake is to choose a pasteurizer first and then try to bend the product around it.
Start with the product specification instead.
| Product | Important Characteristics | Typical Processing Concerns |
| Milk | Low viscosity, protein-rich, relatively heat-sensitive | Microbial safety, fouling, flavor quality |
| Flavored milk | Milk plus sugar/flavoring | Fouling, viscosity, formulation |
| Cream | Higher fat content and viscosity | Heat transfer, flow stability |
| Fruit juice | Often acidic, may contain pulp or particles | Flavor, color, particle handling |
| Soy milk | Plant protein, low-acid | Protein stability, fouling |
| Oat beverage | Suspended solids, starch/protein | Viscosity, heat sensitivity, fouling |
| Nut-based beverage | Fat, protein, fine particles | Separation, fouling, texture |
| Tea/coffee beverages | Heat-sensitive flavor compounds | Flavor retention, oxidation |
The product determines the appropriate temperature-time combination and, just as importantly, the type of heat-transfer equipment that can deliver it consistently.
A low-viscosity liquid with little suspended material is generally easier to push through a plate heat exchanger. A thicker product, or one carrying particles, may need a different flow path and heat exchanger design.
HTST vs. UHT: What Is the Difference?
One of the first decisions is whether the product requires high-temperature short-time (HTST) pasteurization or ultra-high-temperature (UHT) treatment.

HTST Pasteurization
HTST uses a relatively high temperature for a short holding period. After the required treatment, the product is rapidly cooled.
For refrigerated milk and similar products, the objective is generally to hit the required microbial reduction while keeping the sensory and nutritional characteristics buyers expect.
HTST is commonly associated with:
- Fresh milk
- Flavored milk
- Cream
- Yogurt drinks
- Some refrigerated beverages
The exact processing temperature and holding time must be established according to the product, applicable regulations, and process validation requirements, not from one universal setting.
UHT Processing
UHT uses a substantially higher temperature for a very short time and is designed for products requiring much greater commercial sterility when combined with appropriate hygienic or aseptic processing and packaging.
It is commonly considered for:
- Long-life milk
- Formulated dairy beverages
- Soy milk
- Certain plant-based beverages
- Some juice and tea/coffee applications
Keep one thing straight: UHT is not simply “stronger pasteurization.” It belongs to a different processing and packaging strategy.
Plate Pasteurizers: When Are They a Good Choice?
Plate heat exchangers are widely used for relatively fluid products because they deliver efficient heat transfer in a compact footprint.
A typical plate pasteurization system can include:
- Product balance tank
- Feed pump
- Regeneration section
- Heating section
- Holding tube
- Cooling section
- Flow-diversion system
- Temperature and flow controls
The regeneration section earns its keep here: outgoing hot product transfers heat to incoming cold product, which cuts the external heating and cooling load.
For example, Zhongbo’s Plate Pasteurizer is specified for pasteurization temperatures up to 140°C, processing times of 5–30 seconds, and capacities from 300 to 10,000 L/h. The manufacturer lists applications including milk, flavored milk, cream, yogurt drinks, formulated dairy products, soy milk, juice, tea, and coffee.
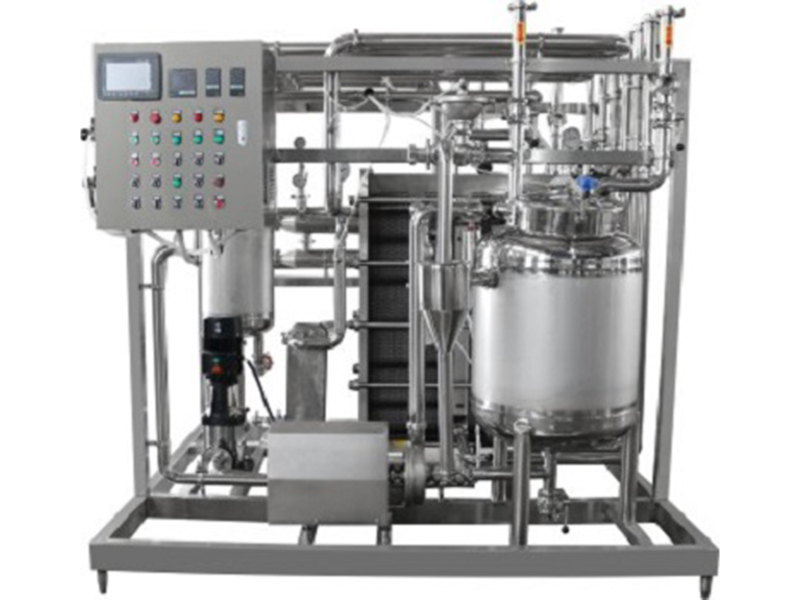
Plate systems are particularly attractive when:
- The product has relatively low viscosity.
- Suspended particles are limited.
- High heat-transfer efficiency is important.
- Production capacity is moderate to high.
- A compact heat-exchange system is preferred.
Product formulation still matters, though. A beverage with significant particles or higher viscosity may need a different heat exchanger configuration.
Tubular Pasteurizers: When Should You Consider Them?
Tubular systems move product through tubes rather than narrow plate channels.
That open structure is what makes tubular technology attractive for products that are more viscous or harder to run through conventional plate channels.
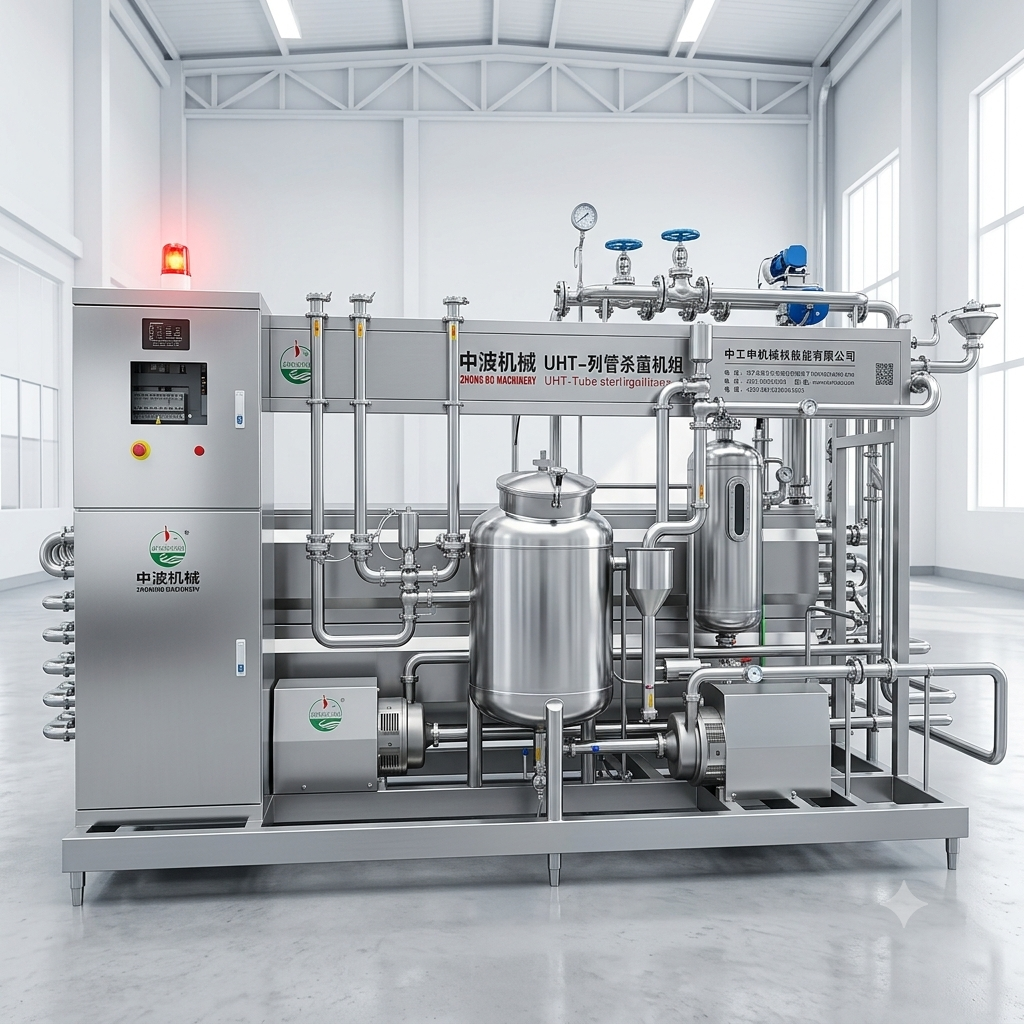
A typical tubular pasteurizer may include:
- Balance tank
- Product feed pump
- Flow-control system
- Tubular heat exchanger
- Regeneration section
- Heating section
- Holding section
- Cooling section
- Flow-diversion valves
- Instrumentation and controls
According to Zhongbo’s Tubular Pasteurizer page, its tubular system is designed for temperatures up to 140°C, treatment times of 5–300 seconds, and capacities from 300 to 10,000 L/h. The company specifically notes its suitability for viscous liquid materials and applications including dairy products, soy milk, juice, tea, and coffee. (浙江中博)
Tubular systems may be considered when:
- Product viscosity is relatively high.
- The beverage contains suspended material.
- Fouling behavior makes another configuration less suitable.
- The process requires a longer holding time.
- A more flexible product-handling configuration is needed.
That doesn’t mean “tubular is always better.” The right choice depends on the actual rheology, particle size, concentration, flow rate, and heat-transfer requirements.
Milk, Juice, and Plant-Based Beverages Need Different Considerations
Milk
Milk is relatively fluid, but it carries proteins, fat, minerals, and other components that interact with heated surfaces.
The major concerns are:
- Microbial safety
- Protein denaturation
- Fouling
- Heat recovery
- Flavor quality
- Accurate temperature and holding-time control
For many milk applications, a plate pasteurizer provides efficient heat transfer in compact equipment.
For higher-temperature treatment or more demanding formulations, a tubular configuration may be considered.
Fruit Juice
Juice brings a different set of considerations.
Many fruit juices are acidic, which changes their microbial stability compared with low-acid products. Acidity does not remove the need for controlled thermal processing.
The processor should consider:
- pH
- Fruit type
- Pulp or fiber content
- Particle size
- Viscosity
- Color and flavor sensitivity
- Dissolved oxygen
- Desired shelf life
- Filling and packaging method
Clear apple juice, orange juice with pulp, and a concentrated fruit beverage may need very different process designs even though all of them get filed under “juice.”
For beverages containing pulp or suspended particles, the heat exchanger must provide suitable flow conditions without damaging the product.
Plant-Based Beverages
Plant-based beverages are worth special attention because their formulations vary so much.
Soy, oat, almond, coconut, pea, and mixed-grain beverages can differ significantly in:
- Protein content
- Fat content
- Starch content
- Particle concentration
- Viscosity
- Sedimentation behavior
- Heat stability
A soy beverage can behave differently from an oat beverage during heating, for example, because their protein and starch systems are not the same.
So the pasteurization system should be selected together with the formulation and the upstream homogenization/mixing process, not as an isolated piece of equipment.
A Practical Selection Matrix
The following framework can help narrow down the options:
| Factor | Plate System | Tubular System |
| Low-viscosity milk | Very suitable | Suitable |
| Flavored milk | Suitable | Suitable |
| Cream | Depends on formulation | Often worth considering |
| Clear juice | Suitable | Suitable |
| Juice with particles | Depends on particle characteristics | Often worth considering |
| Soy beverage | Suitable | Suitable |
| Higher-viscosity plant beverage | Product-dependent | Often worth considering |
| Compact design | Strong advantage | Depends on configuration |
| Heat-transfer efficiency | High | High, depending on design |
| Viscous products | Product-dependent | Often more flexible |
| Fouling management | Important | Important |
Treat the table as a preliminary screening tool, not an equipment-selection rule.
Actual selection should be based on product testing and process calculations.
Don’t Ignore Fouling
Fouling is one of the most practical issues in thermal processing.
Milk proteins, minerals, sugars, plant proteins, starches, and other components deposit on heat-transfer surfaces. As deposits accumulate:
- Heat-transfer efficiency decreases.
- Pressure drop can increase.
- Product temperature control becomes more difficult.
- Cleaning frequency may increase.
- Production downtime can rise.
This hits plant-based beverages hardest, because their formulations often combine protein, starch, oil, minerals, and stabilizers.
So ask the equipment manufacturer:
How does the proposed system handle this specific product’s fouling behavior?
Don’t rely on general equipment specifications alone.
Zhongbo’s tubular pasteurizer information, for example, specifically mentions fouling control and cleaning solutions as part of the system design.
Consider the Entire Process Line
Pasteurization should not be designed in isolation from the rest of the beverage line.
A typical system may involve:
Raw material → filtration/separation → mixing → homogenization → pasteurization → cooling → buffer/storage → filling
Depending on the product, additional operations may be required. A plant-based beverage may need intensive mixing before thermal treatment, while a fruit beverage may need particle management and deaeration.
The pasteurizer also needs compatible:
- Pumps
- Holding tubes
- Valves
- Temperature sensors
- Flow meters
- Control systems
- CIP connections
- Heating utilities
- Cooling utilities
- Product storage or buffer tanks
Zhongbo’s product range includes pasteurization equipment as well as stainless steel pumps, mixing tanks, buffer tanks, heat exchangers, and CIP equipment, so these process components can be considered as part of a larger processing system.
What Information Should You Give the Equipment Manufacturer?
Before requesting a quotation, prepare as much of the following information as possible:
Product information
- Product name
- Ingredients
- pH
- Viscosity
- Total solids
- Fat/protein content
- Particle size and concentration
- Temperature before treatment
Production requirements
- Target capacity, such as L/h
- Batch or continuous operation
- Operating hours per day
- Required treatment temperature
- Required holding time
- Inlet and outlet temperatures
Packaging and shelf life
- Refrigerated or ambient distribution
- Bottle, carton, pouch, or other packaging
- Hot filling, aseptic filling, or conventional filling
- Target shelf life
Utilities
- Steam availability
- Electricity
- Cooling water
- Compressed air
- Plant water temperature
The more complete this information is, the less likely it is that the equipment selection will be based on assumptions.
Common Mistakes When Choosing a Pasteurization Method
Choosing equipment based only on capacity
Two systems may both process 5,000 L/h and still behave very differently with different products.
Looking only at maximum temperature
A pasteurizer rated for 140°C is not automatically suitable for every product that needs high-temperature treatment.
Ignoring viscosity
A beverage that looks like milk can flow completely differently once you add protein, starch, or solids.
Forgetting CIP requirements
A system that processes the product well but is hard to clean will create operating problems down the line.
Treating all plant-based beverages as one category
Soy, oat, almond, pea, and coconut beverages can differ substantially in thermal-processing behavior.
Selecting the pasteurizer before defining the product
The process should drive the equipment design, not the other way around.
Q&A: Choosing the Right Pasteurization Method
- Is a plate pasteurizer suitable for milk?
Yes. Plate heat exchangers are widely suited to fluid dairy products, and their compact design and efficient heat transfer make them a common option for milk processing. The actual configuration should follow the required treatment conditions and production capacity.
- Is tubular pasteurization better for plant-based beverages?
Not automatically. Some plant-based beverages benefit from tubular processing because of viscosity, suspended solids, or fouling characteristics, but the choice should rest on the actual formulation and process requirements.
- Can the same pasteurizer process milk and juice?
Potentially, yes. Equipment can be designed for multiple products, but product properties, cleaning requirements, temperature programs, and changeover procedures all have to be worked through.
- What is the main difference between HTST and UHT?
HTST uses a relatively high temperature for a short holding period and is commonly associated with refrigerated products. UHT uses a higher-temperature, very-short-time process and is generally paired with longer shelf-life products when combined with suitable hygienic or aseptic packaging.
- Does juice always need UHT treatment?
No. The appropriate thermal process depends on juice acidity, microbial targets, formulation, packaging, and desired shelf life.
- Why is viscosity important when choosing a pasteurizer?
Viscosity affects flow behavior, pressure drop, heat transfer, pumping, and which heat-exchanger configurations will actually work.
- How does fouling affect pasteurization?
Deposits on heat-transfer surfaces reduce heat-transfer performance and can increase pressure drop and cleaning requirements. Fouling behavior should therefore be part of equipment selection.
- What capacity can a pasteurizer handle?
Capacity depends on the equipment design. For example, Zhongbo lists both its plate and tubular pasteurizer systems in the range of 300–10,000 L/h, with the appropriate configuration depending on the application.
- Should I choose plate or tubular equipment first?
Neither should be chosen on the equipment name alone. Start with the product, processing conditions, capacity, viscosity, particle characteristics, heating/cooling requirements, and cleaning requirements. Then pick the heat-transfer configuration that fits.
Conclusion
Choosing the right pasteurization method for milk, juice, or plant-based beverages takes more than comparing temperature ratings or equipment capacity.
The key questions are:
- What is the product?
- What are its pH, viscosity, solids, and particle characteristics?
- What temperature-time treatment is required?
- Is the product refrigerated or shelf-stable?
- How much fouling is expected?
- What production capacity is needed?
- How will the system be cleaned and integrated with the rest of the processing line?
Plate pasteurizers can be an efficient choice for many relatively fluid products, while tubular systems offer more flexibility for certain viscous or particle-containing products. The final decision should rest on actual process data, not on a generic “one machine fits all” approach.
Zhejiang Zhongbo Mechanical Technology Co., Ltd. provides pasteurization and related dairy and beverage processing equipment, including plate and tubular systems. If you are planning a new milk, juice, or plant-based beverage line, sharing your product formulation, capacity, treatment requirements, and packaging method with the equipment manufacturer is a practical starting point for developing the right process configuration.